 Thermal Technologies
Industry
Rubber and Elastomers
Curing and vulcanising platens, extruder barrels and mould heating.
Long soaks at temperature, big platens, and cure that depends on the whole face being even.
The process, and where the heat goes in
Read left to right. Each block is a place on the machine that has to be held at a temperature, coloured by how hot it runs.
Scroll the diagram sideways to see every zone.
- Coolest
- Warm
- Hot
- Hottest
Zone by zone
This table is the whole argument for the page. It maps the machine you already have to the element type that suits each position on it, and every product name links to the family page with the sizes, the options and the codes.
| Zone | Duty | Typical temperature | Swiftheat product | Why this element |
|---|---|---|---|---|
| Curing and vulcanising platens | Embedded, continuous | 140 to 220 °C | Cartridge Heaters | Bore mounted across the platen, wattage distributed for an even face |
| Moulds and bolsters | Embedded | 140 to 200 °C | Cartridge Heaters | Sized to the bores already in the tool |
| Extruder barrel | Banded surface, continuous | 60 to 120 °C | Ceramic and Mica Band and Nozzle Heaters | Rubber barrels run cooler than plastics, so watt density is lower |
| Preheat and warm up | Radiant or air | 40 to 120 °C | Ceramic Infrared Heaters | Brings stock and tooling up before the run starts |
| Control loop | Measurement | - | Thermocouples and Temperature Sensors | Platen sensors sized to the bores already drilled |
Temperatures are typical for the process and are given as a starting point. Send us the zone temperatures your machine actually runs at and we will work back to a safe loading.
Products for rubber and elastomers
A shortlist, not the whole catalogue.
-
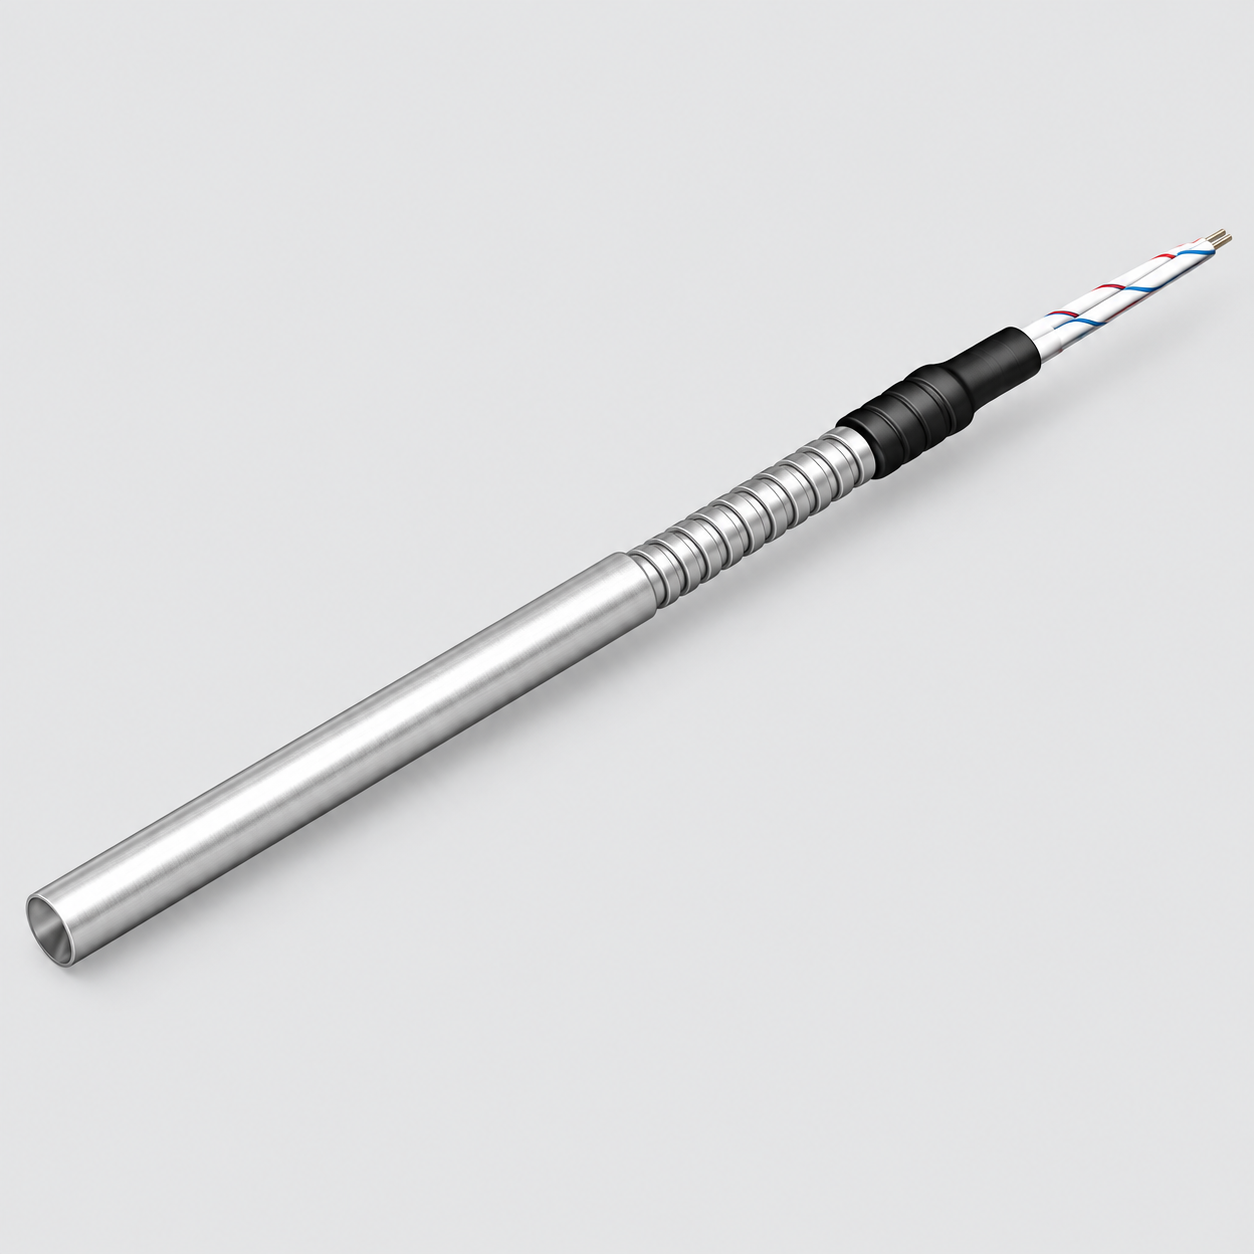 Cartridge Heaters
Bore mounted in moulds, platens and dies. Round, swaged, made to your length.
-
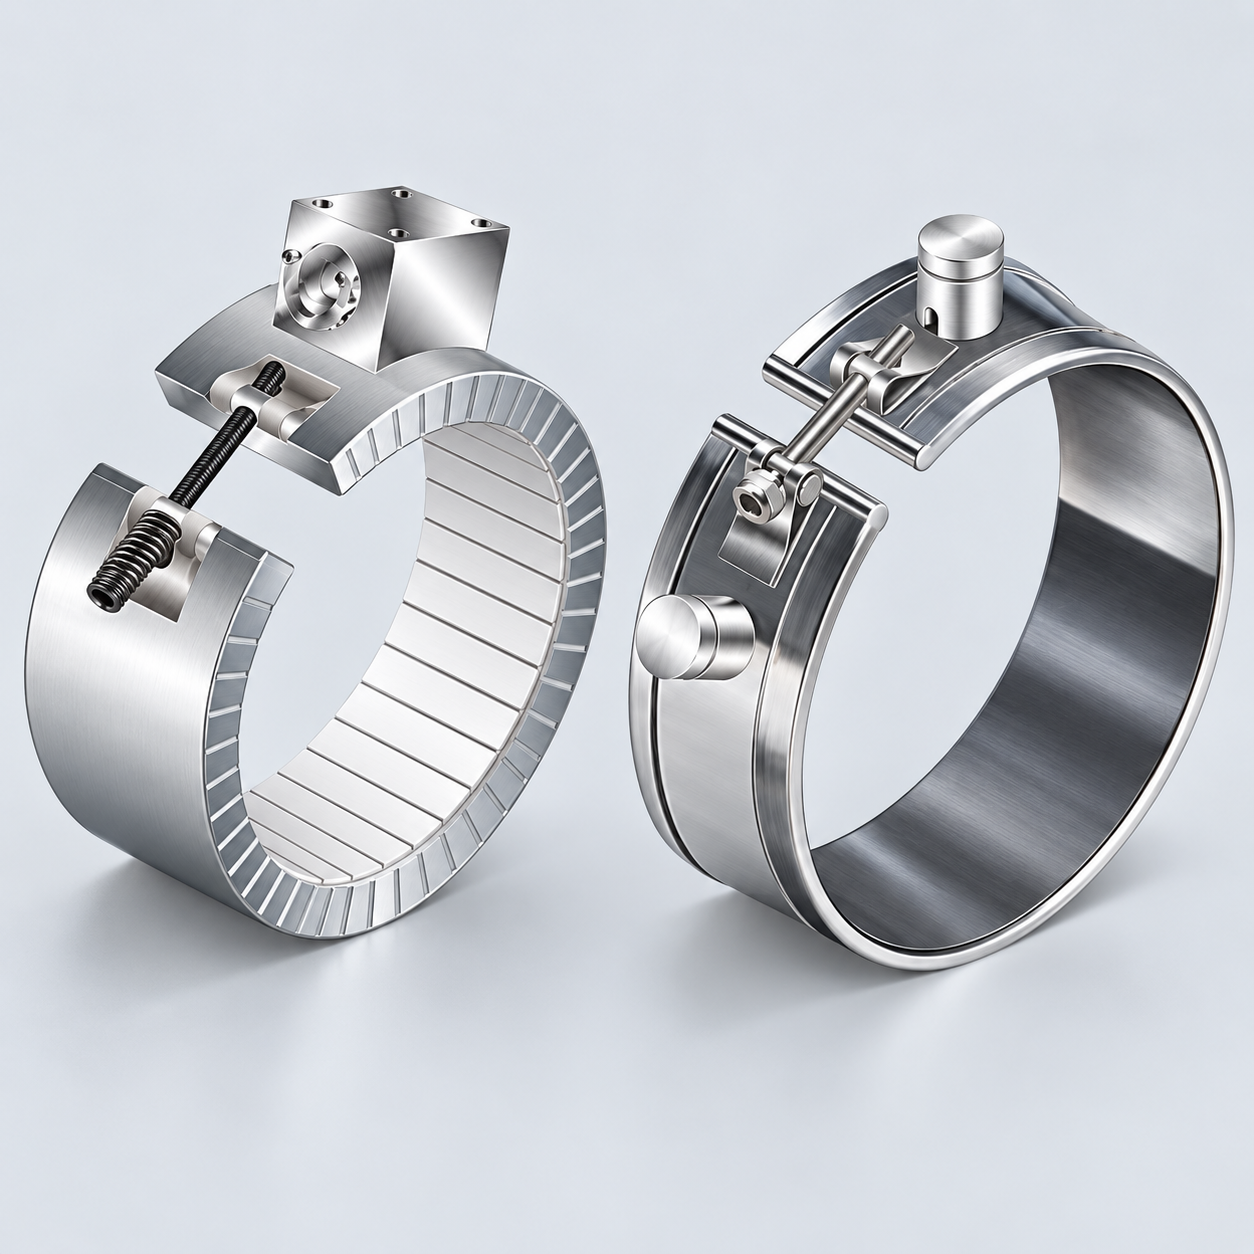 Ceramic and Mica Band and Nozzle Heaters
Barrels, cylinders, pipes and injection nozzles. One piece, split, expandable or partial coverage.
-
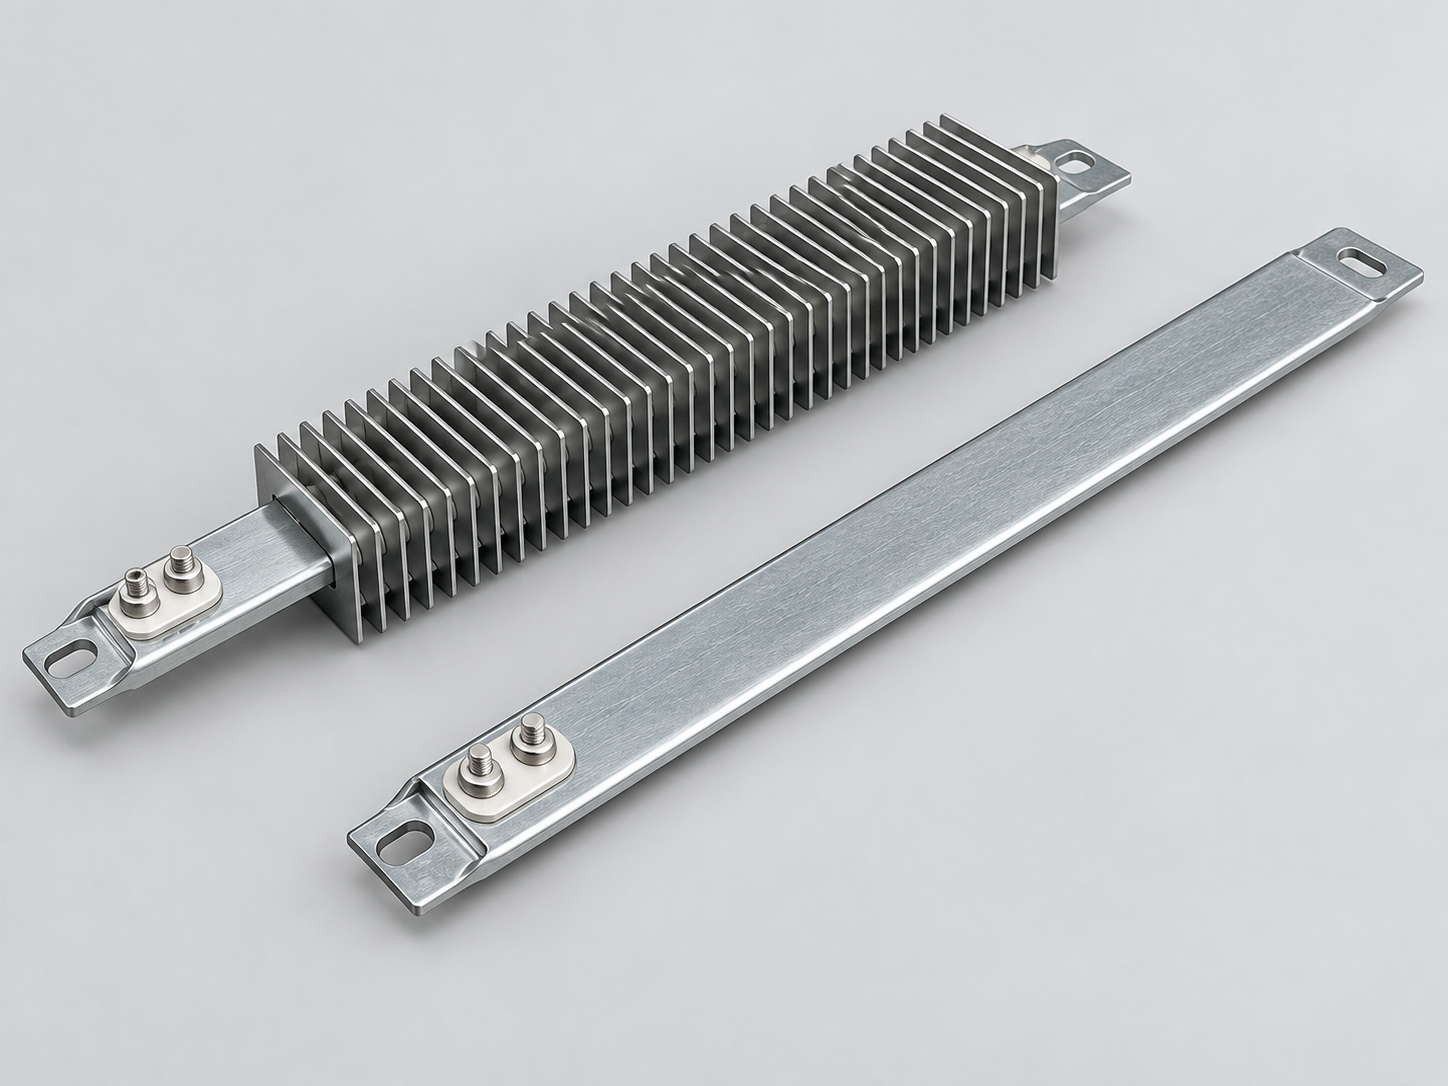 Strip Heaters
Flat and gently curved surfaces, sealing bars, platens and duct air.
-
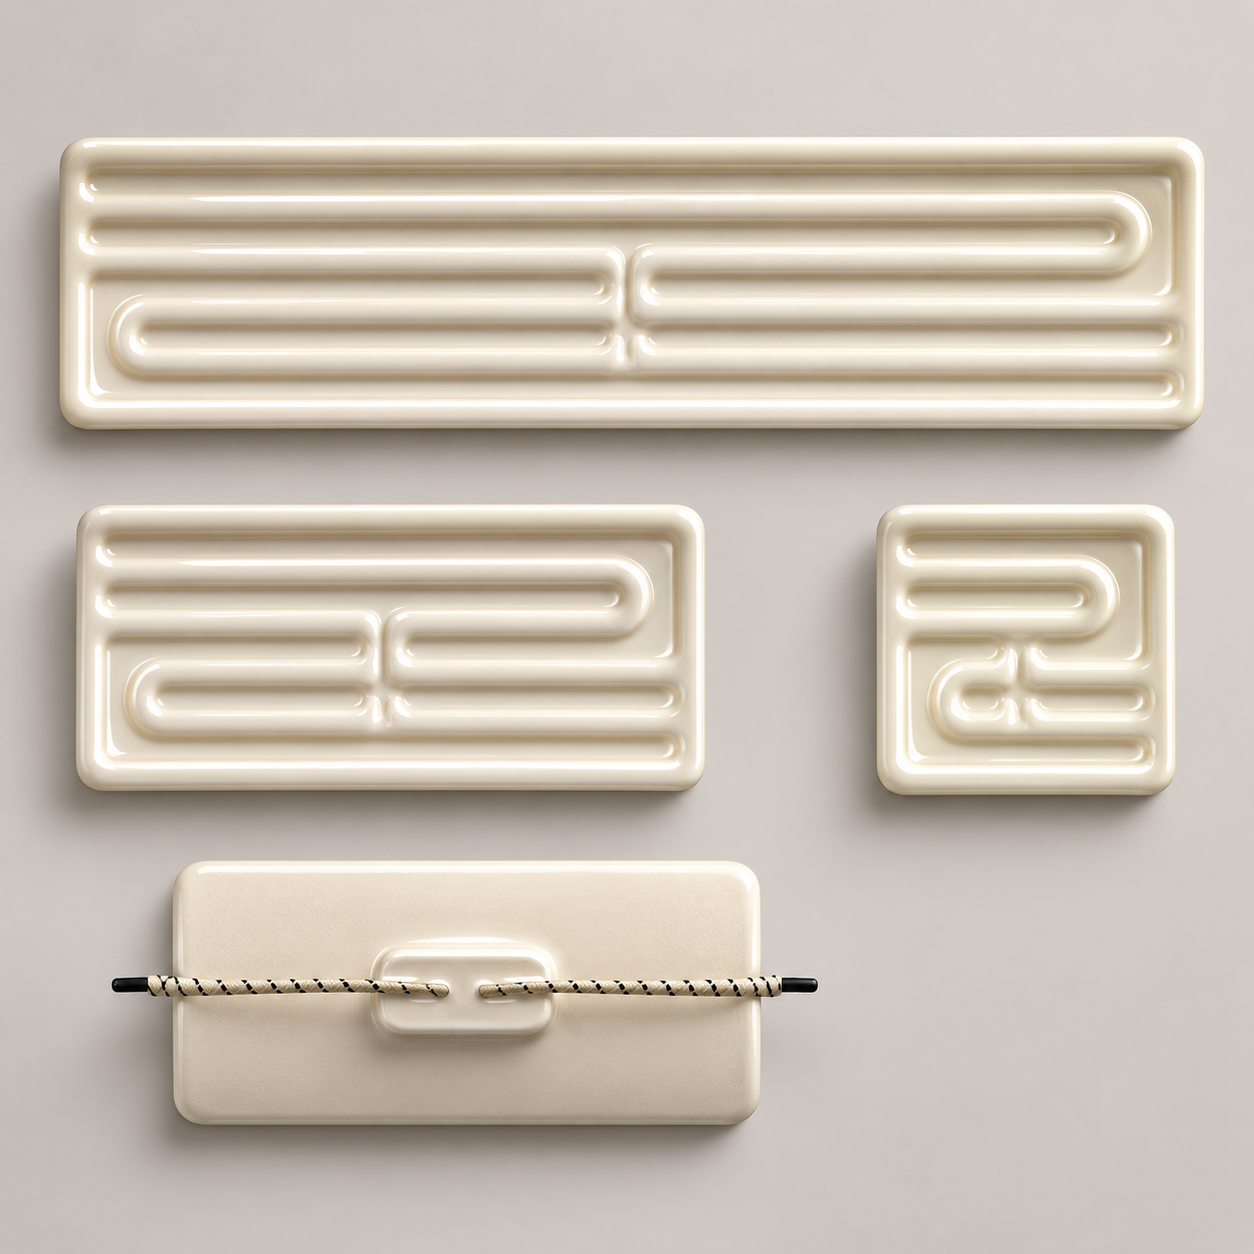 Ceramic Infrared Heaters
Radiant surface heating, thermoforming, drying and preheating.
-
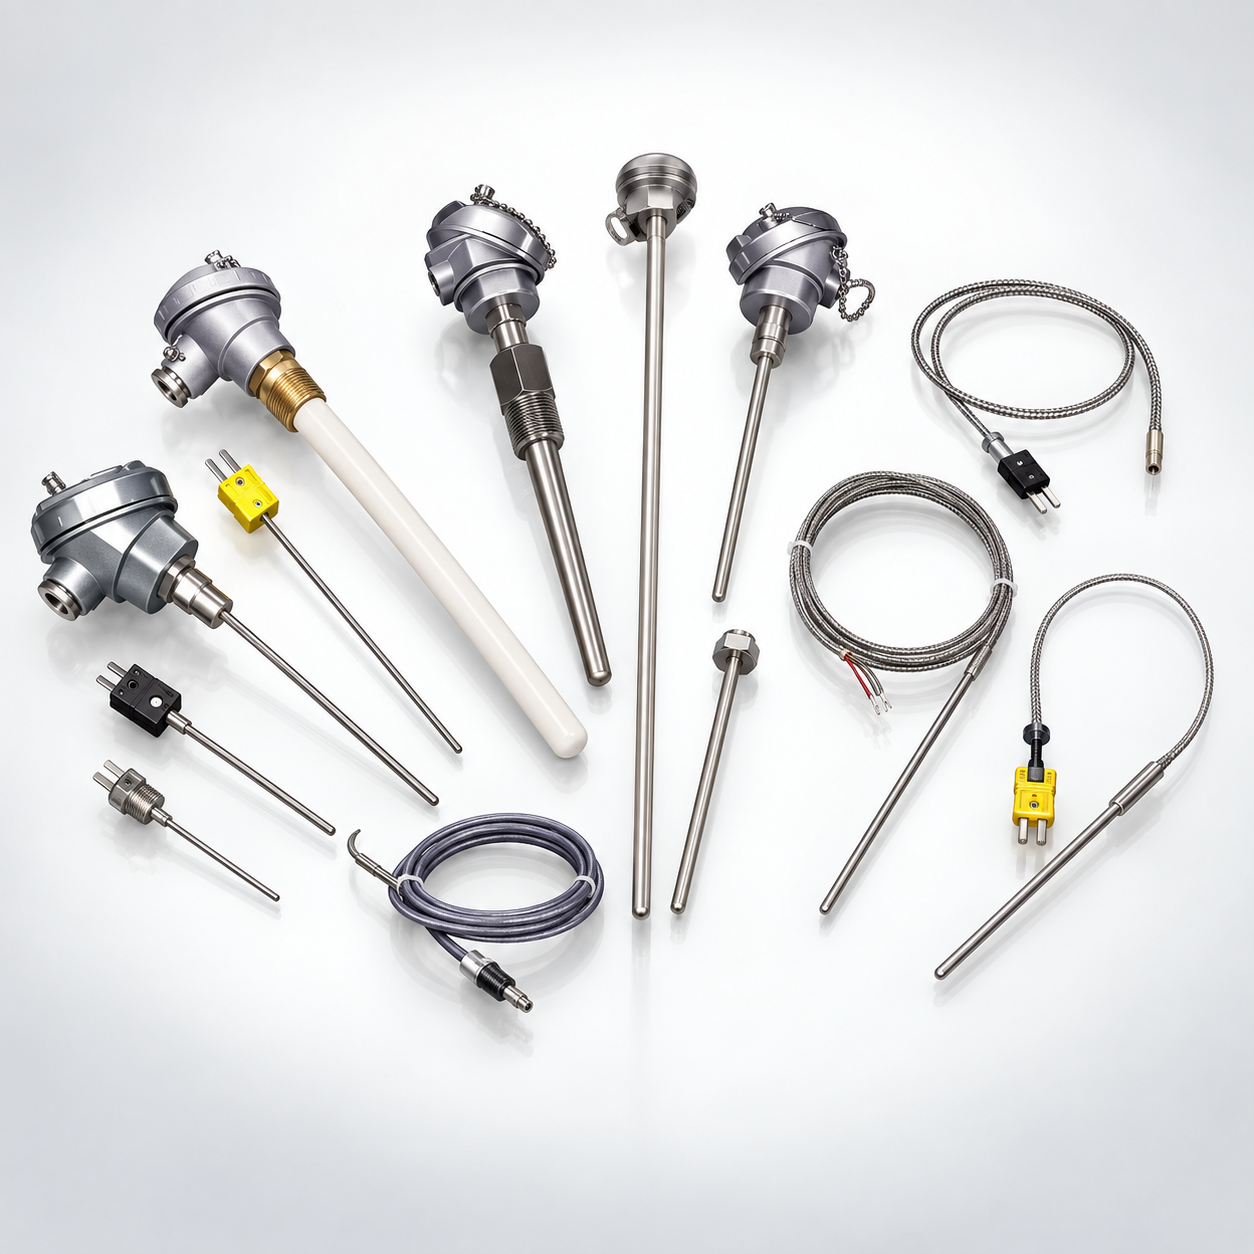 Thermocouples and Temperature Sensors
Types J, K, N, T, E, R, S, B and C, plus PT100, PT500 and PT1000 RTDs, made to length.
Application notes
Cure is decided by the coldest point on the platen
The whole face has to be within the cure window, so the specification is the spread across the platen, not the average. Tell us the platen size, the bore layout and the spread you have to hold.
Rubber barrels are not plastics barrels
An extruder running rubber works at a much lower temperature than one running plastics, and it wants a lower watt density to match. Reusing a plastics band specification here shortens element life for no benefit.
Long soaks favour a conservative loading
Rubber tooling sits at temperature for hours at a time. A heater specified conservatively is cheaper over a year than one specified for the fastest possible heat up.
What to send us
An enquiry with these in it can be quoted the same day. An enquiry without them takes three phone calls first.
- Process: compression, transfer, injection or extrusion
- Platen or tool dimensions and the bore layout
- Bore diameter, tolerance and depth
- Cure temperature and the spread the process allows
- Hours at temperature per day
- Barrel diameter and zone widths for extrusion
A photograph of the old element next to a tape measure is worth more than a paragraph of description, and a drawing is worth more than both.
Build the list instead
If you are replacing several elements at once, the list builder walks through each one, draws it as you specify it, and produces a single printable document you can send by email or on WhatsApp.
Request a quote for rubber and elastomers
Tell us the machine and the zone. If you are not sure which element type suits it, leave the product blank and our engineers will propose one.